
China High-Efficiency Brine Concentration Systems from China Suppliers - Advanced Factory Solutions for Wastewater Treatment Factories, Manufacturer
Product Description
Core Features
⚡ Low Energy Consumption & High Concentration Ratio
The fully membrane-based concentration technology achieves a specific energy consumption of only 7–11 kWh/m³, comparable to conventional seawater RO membranes. It saves over 70% energy compared to traditional evaporation methods. For a 1,000 m³/day capacity, evaporation load can be reduced by 60%–80%, saving millions of CNY annually.
🚚 Flexible Skid-Mounted Deployment & Intelligent O&M
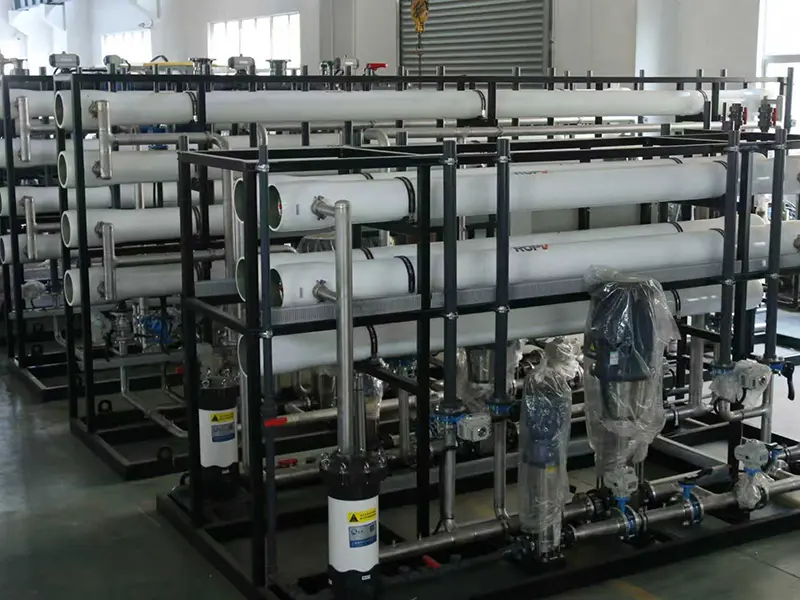
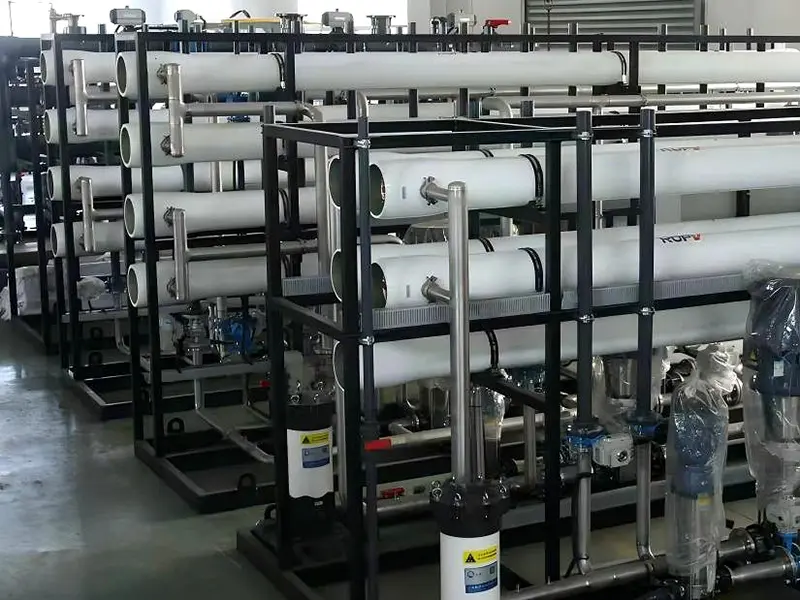
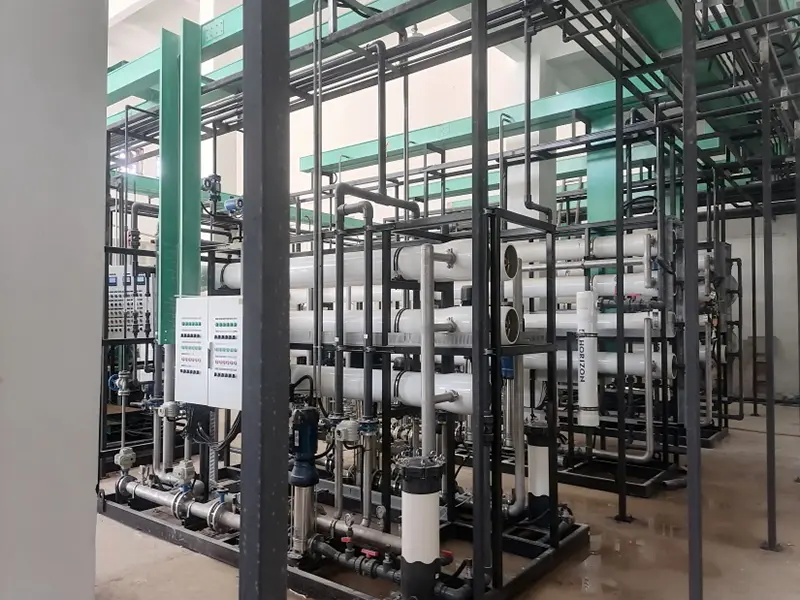
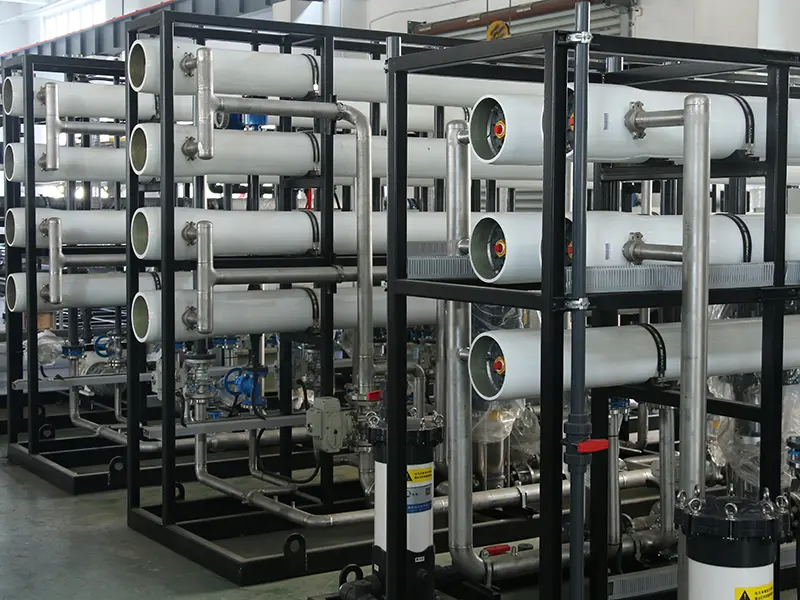
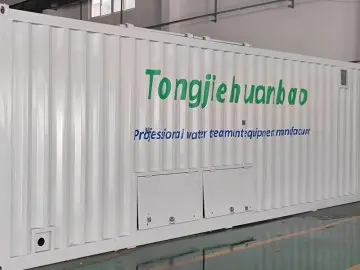
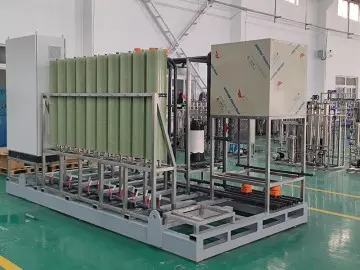
Standard containerized skid modules allow integrated installation and relocation. Integrates PLC intelligent control and IP65 protection, adapting to extreme conditions. The system includes online performance monitoring for real-time tracking of individual membrane modules.
📈 High-Ratio Concentration Capability
TDS can be concentrated from tens of thousands mg/L to over 210,000 mg/L, approaching sodium chloride saturation. This creates optimal conditions for resource recovery and significantly reduces the size of required evaporation crystallizers.
📍 Modular Design
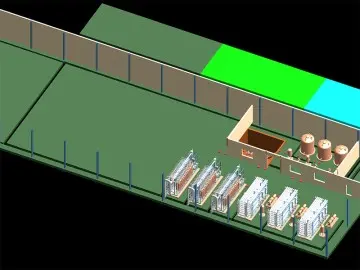
Capacities from 0.5 to 500 m³/h. Supports multiple skids in parallel for expansion, meeting needs from single factories to large industrial parks.
♻️ Resource Recovery
Coupled with nanofiltration, it recovers sodium chloride and sodium sulfate as industrial-grade by-products, turning wastewater treatment into a profit center.
Application Fields
🏭 Chemical Industrial Parks
Zero Liquid Discharge (ZLD) for high-salinity wastewater, concentrating to over 210,000 mg/L.
⚙️ Electroplating Industry
Reduces concentrate volume by up to 80%, increasing recovery rates of valuable product water.
🧪 Textile & Pharma
Salt separation and recovery of sodium chloride and sulfate for industrial resale.
⛏️ Coal Chemical ZLD
Doubles treatment capacity of existing systems without adding new evaporator units.
🚨 Emergency Compliance
Rapid on-site deployment within 1–7 days for environmental inspection rectification.
🔩 Steel & Non-Ferrous
Enrichment and recovery of valuable metal ions like sodium and potassium.
Other Products
Send Inquiry
Frequently Asked Questions
Our system consumes only 7–11 kWh/m³, which represents over 70% energy savings compared to traditional thermal evaporation methods.
The system can concentrate high-salinity wastewater to over 210,000 mg/L TDS, approaching the saturation point of sodium chloride.
Thanks to our skid-mounted containerized design, on-site deployment can be completed within 1 to 7 days, making it ideal for emergency rectification.
Yes. By coupling it with nanofiltration technology, we can separate and recover industrial-grade salts like sodium chloride and sodium sulfate for resale.
We provide a full series of modular units with capacities ranging from 0.5 m³/h to 500 m³/h, which can be scaled in parallel.
Yes, the equipment features IP65 protection and PLC intelligent control, designed for unattended operation in harsh industrial environments.









