ODM China Food & Beverage Process Water System - Reliable Suppliers and Factory Solutions for Purified Water Factory, Manufacturers

,

Water Quality is Key to Product Excellence – Purified Water is Essential for Food and Beverage Production.
In the food and beverage industry, from ingredient mixing to equipment cleaning and final bottling, every drop of water impacts taste, safety, and shelf life. Our advanced purification system, utilizing two-stage reverse osmosis (RO) and deep disinfection technology, ensures the production of water that consistently complies with GB 5749, GB 19298, and other national food safety standards. This process effectively eliminates microorganisms, heavy metals, residual chlorine, and organic contaminants at the source, delivering safe, stable, and cost-effective purified water tailored for food and beverage enterprises. As a leading supplier in China, our factory is dedicated to providing superior water solutions that meet the stringent requirements of the industry.

,

Product Description

✓

Product Description

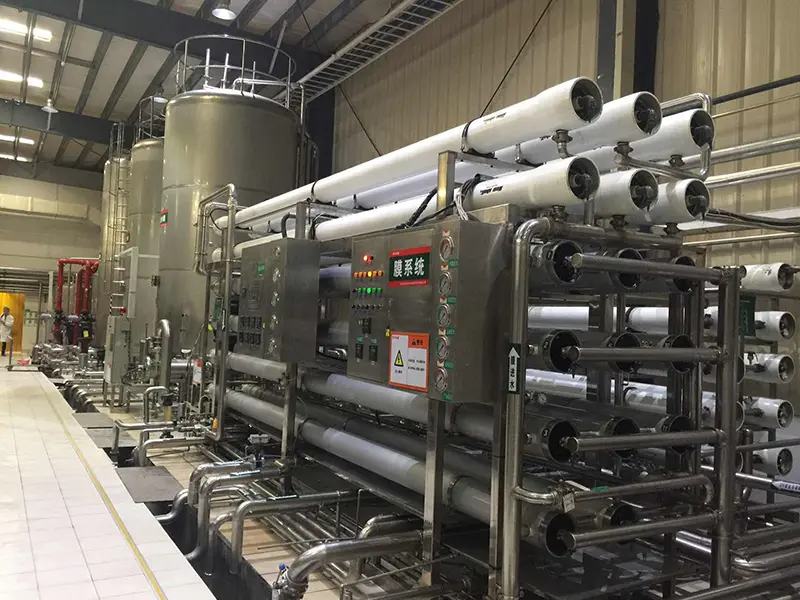
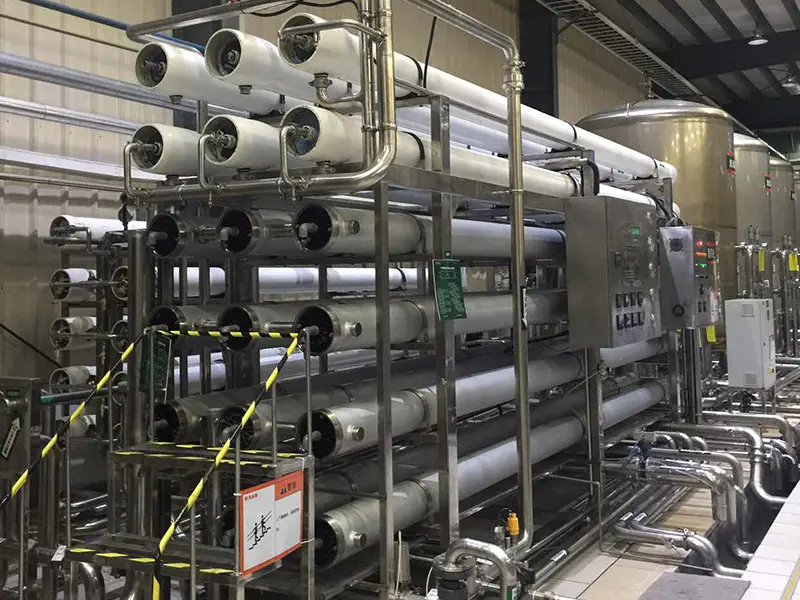
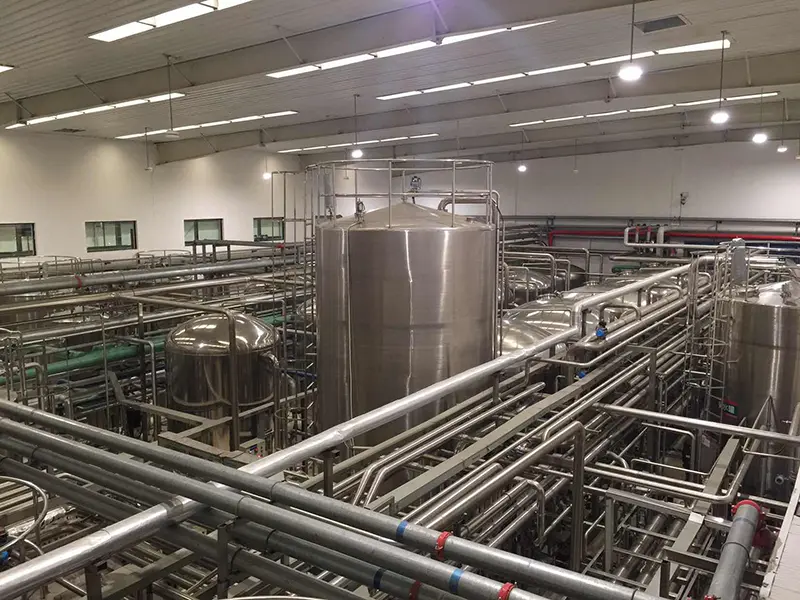
This purified water system is a complete water treatment solution designed specifically for the food & beverage industry. Built around two-stage reverse osmosis (RO), it integrates pretreatment, fine filtration, disinfection and intelligent control — delivering “raw water in, purified water out” fully automatically.

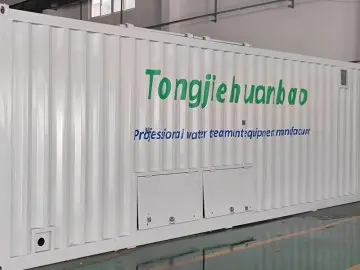
Food & Beverage Process Water System 1
Food & Beverage Process Water System 2
Standard Process Flow

Raw water → Raw water tank → Booster pump → Multimedia filter → Activated carbon filter → Water softener (optional) → Cartridge filter → 1st pass RO → 2nd pass RO → UV sterilizer / ozone generator → Stainless steel sterile pure water tank → Distribution points.

Product Water Quality

Conductivity consistently ≤ 10 μS/cm (customisable to ≤ 1 μS/cm); Desalination rate ≥ 98%; Microorganisms, heavy metals, residual chlorine etc. fully comply with food processing & packaged drinking water standards.

Capacity Range

1 – 100 tonnes per hour, modular design for easy customisation and future expansion.

Control Mode

PLC fully automatic control + 7” touch screen; realtime monitoring of conductivity, flow rate, pressure, pH, etc.; remote monitoring & automatic alarm available.

An ideal solution for meeting short-term or long-term decentralized water supply demands

Contact Now
★

Advantage Technical Highlights

Advantage Technical Highlights
High desalination rate Twopass RO system achieves ≥98% desalination, effectively removing dissolved salts, heavy metals, bacteria and organic compounds.
Consistent compliance Product water conductivity can be as low as ≤1 μS/cm, meeting GB 5749, GB 19298, GB 14881 and other food safety standards.
High recovery rate System recovery 50%~80%; concentrate can be reclaimed to save water and reduce discharge.
Food grade materials Piping and storage tanks made of 304/316L hygienic stainless steel, quickconnect joints, deadlegfree design, supports CIP cleaning.
Double disinfection 254 nm UV sterilisation (≥99.9% kill rate) + ozone mixing, eliminates microbial recontamination.
Smart control PLC + IoT remote monitoring; automatic alarm and discharge if water quality exceeds limit; RO membranes autoflushed at set intervals to prolong membrane life.
Low operating cost Energy consumption approx. 2.5–4.5 kWh/m³ produced; long consumable replacement cycle; 25%~35% lower O&M cost compared to conventional processes.
Flexible customisation Options for highhardness water, high residual chlorine, high microbial load etc. — e.g. extra softening, enhanced activated carbon, UV+ozone combination.
📍

Application Areas

💧
Packaged drinking water: Meet GB 19298 standard for purified/mineral water.
🍹
Beverages & fruit juices: Ensure pure taste and no precipitation in drinks.
🥛
Dairy & plant protein: Prevent scaling and microbial contamination.
🍺
Alcoholic & brewing: Stabilise fermentation and improve clarity.
🍶
Condiments: Avoid off-flavours in soy sauce, vinegar, and sauces.
🧼
Food processing cleaning: Final rinse for equipment and pipelines.
❄️
Ice making & cooling: Eliminate hygiene risks in catering and baking.
📦

Other Products

Modular Containerized Seawater

Modular Containerized Seawater Desalination
ZLD System

Wastewater Volume Reduction & ZLD System
OEM Manufacturing

OEM Precision Manufacturing

ODM Innovation

ODM Full Value Chain Innovation

✉

Send Inquiry

?

Frequently Asked Questions

What is the typical water quality produced by this system?
The system utilizes two-stage RO technology to consistently achieve conductivity ≤ 10 μS/cm, and can be customized to reach ≤ 1 μS/cm for high-precision food and beverage requirements.
Does the equipment meet international food safety standards?
Yes, the system is designed with 304/316L hygienic stainless steel and complies with GB 5749, GB 19298, and GB 14881 standards for food processing and packaged drinking water.
What is the capacity range for your purified water systems?
We offer modular designs ranging from 1 to 100 tonnes per hour, allowing for easy customization based on your specific production scale.
How is the system controlled and monitored?
The system features PLC fully automatic control with a 7-inch touch screen. It provides real-time monitoring of conductivity, flow, pressure, and pH, with remote monitoring and automatic alarms available.
How does the system handle microbial contamination?
We employ a double disinfection strategy using 254 nm UV sterilization (≥99.9% kill rate) combined with ozone mixing to ensure the elimination of microbial recontamination in the storage tanks.
Is the system energy efficient?
Yes, the operating cost is low with energy consumption approximately 2.5–4.5 kWh/m³. The system also features high recovery rates (50%-80%) to minimize water waste.

Related Products