OEM High-Efficiency Brine Concentration Systems from China Suppliers | Membrane-Based Factory Solutions Factory, Manufacturers

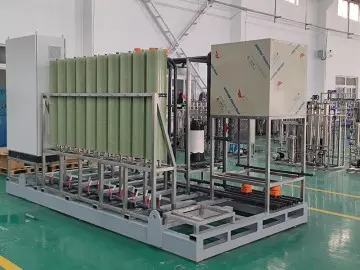
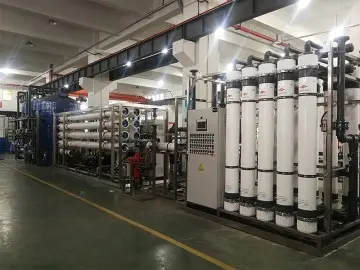
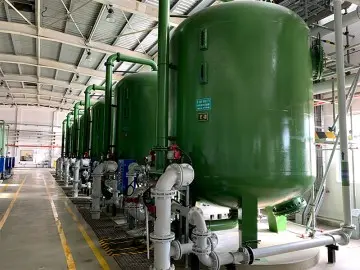
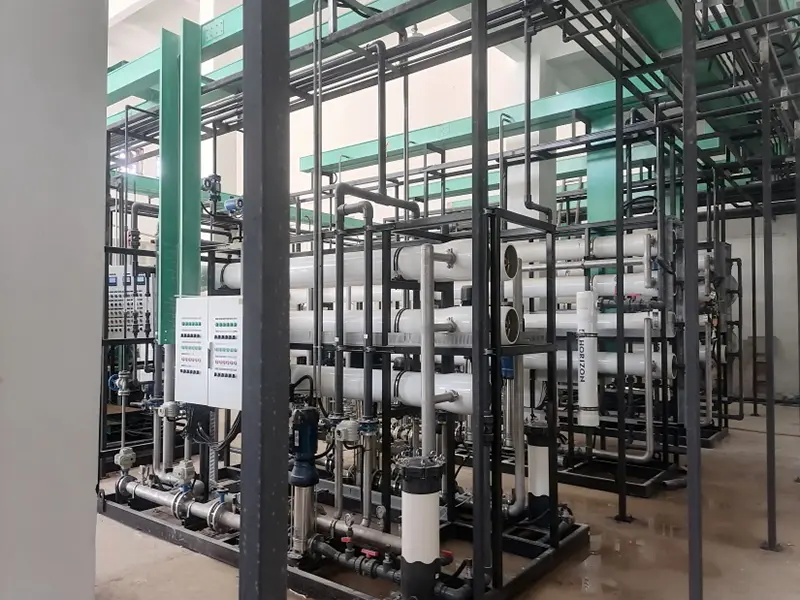
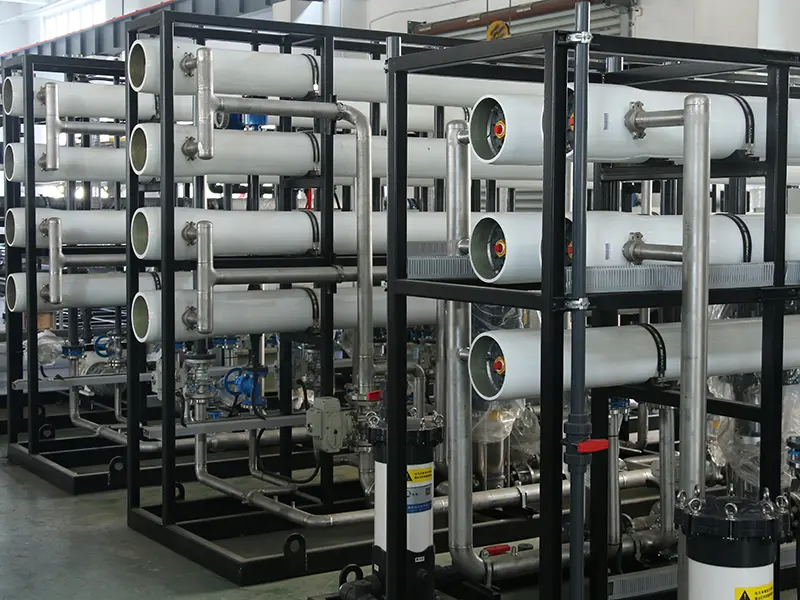
Introducing our state-of-the-art membrane-based brine concentration system, designed for superior efficiency and performance. This skid-mounted unit harnesses advanced osmosis and pressure-driven membrane separation technology to treat high-salinity wastewater from various industries, including chemical, electroplating, textile, pharmaceuticals, and coal chemicals. As a leading China factory and supplier, we provide comprehensive solutions that encompass pretreatment, membrane concentration, deep desalination, and zero-liquid-discharge evaporation, Our innovative system achieves remarkable low-energy performance and can concentrate brine levels up to 210,000 mg/L, dramatically minimizing the space required for evaporators. Operating similarly to seawater reverse osmosis (RO), it produces brine with osmotic pressures exceeding 210,000 mg/L NaCl. This versatile technology is extensively utilized across multiple sectors, including chemicals, power generation, textiles, and rare earth metallurgy, delivering unmatched quality and efficiency. Trust our China-based factory as your reliable supplier for cutting-edge wastewater treatment solutions

Product Description

Core Features

Low Energy Consumption

Low Energy Consumption & High Concentration Ratio

The fully membrane-based concentration technology achieves a specific energy consumption of only 7–11 kWh/m³, comparable to conventional seawater RO membranes, yet delivers a much higher concentration ratio. It saves over 70% energy compared to traditional evaporation methods. For a daily capacity of 1,000 m³, it can save millions of CNY annually in steam and electricity costs.

Flexible Skid-Mounted

Flexible Skid-Mounted Deployment & Intelligent O&M

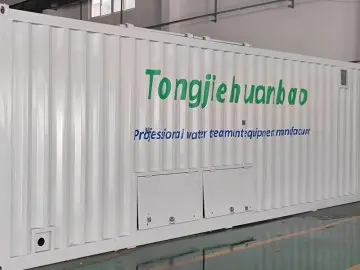
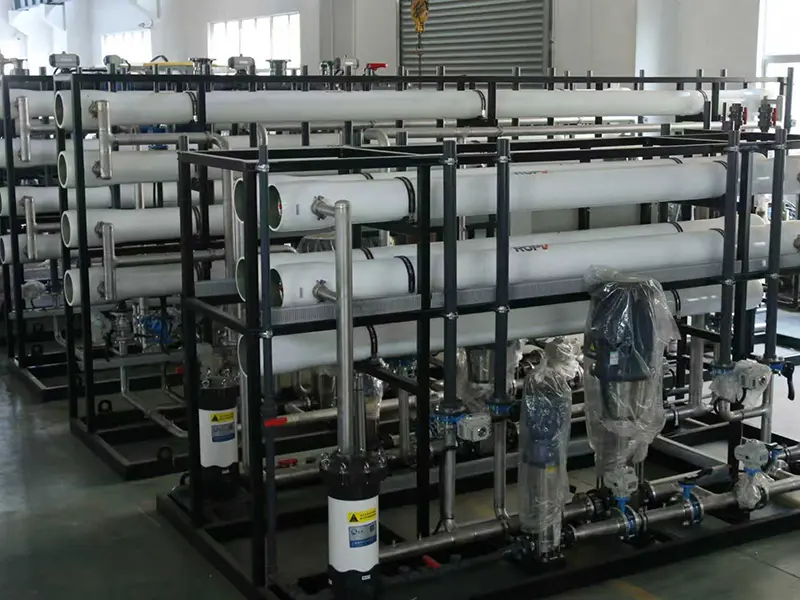
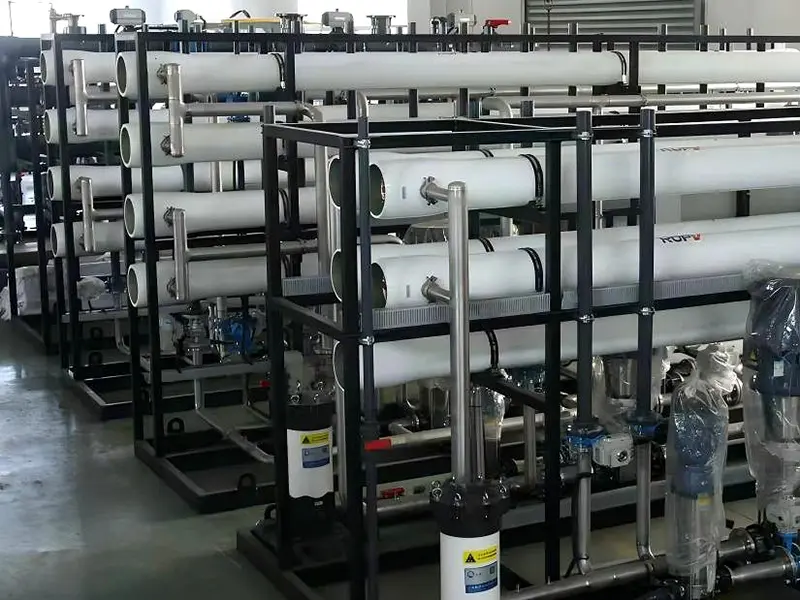
Standard containerized skid modules allow integrated installation and relocation. Integrates PLC intelligent control and IP65 protection, adapting to extreme working conditions. Supports online membrane performance monitoring for real-time tracking and targeted maintenance.

High-Ratio Concentration

High-Ratio Concentration Capability

TDS can be directly concentrated from tens of thousands mg/L to over 210,000 mg/L, approaching the saturation concentration of sodium chloride. This creates optimal conditions for subsequent crystallization or resource recovery while significantly reducing evaporator size.

Modular Design · Scalable on Demand

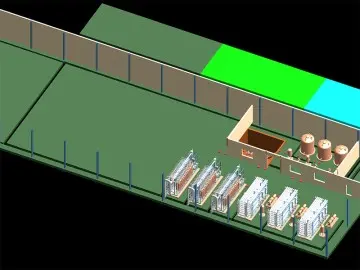
Full series capacities from 0.5 to 500 m³/h are available, supporting multiple skids in parallel for capacity expansion. Actual parameters are custom-optimized based on feed water quality and process routes.

Resource Recovery Orientation

Coupled with nanofiltration salt separation technology, sodium chloride and sodium sulfate can be recovered as industrial-grade salt by-products, transforming wastewater treatment into a profitable resource recovery operation.

An ideal solution for meeting short-term or long-term decentralized water supply demands

Application Fields

Zero Liquid Discharge (ZLD)
Concentrates high-salinity wastewater to over 210,000 mg/L, lowering full-cycle operating costs for chemical industrial parks.
Electroplating Wastewater
Reduces concentrate volume by up to 80%, shortening evaporation steps and increasing valuable product water recovery.
Textile & Pharmaceutical
Combines concentration with nanofiltration to separate and recover industrial-grade salt by-products for sale.
Coal Chemical ZLD Retrofit
Doubles the treatment capacity of existing ZLD systems without adding new evaporator capacity.
Emergency Rectification
Rapid response deployment within 1–7 days to meet environmental inspection requirements and avert production shutdowns.
Steel & Non-Ferrous Metals
Treats concentrated brine to separate and recover valuable metal ions such as sodium and potassium.

Other Products

Modular Containerized Seawater

Modular Seawater Desalination

ZLD System

High-Salinity Wastewater ZLD

OEM Manufacturing

OEM Precision Manufacturing

ODM Innovation

ODM Full Value Chain Innovation

Water Reuse

Water Reuse (UF + RO)

Demineralized Water

Demineralized Water Equipment

Send Inquiry

Frequently Asked Questions

What is the energy saving potential of this system?
The fully membrane-based technology consumes only 7–11 kWh/m³, which is over 70% more energy-efficient than traditional triple-effect falling film evaporators.
How high can the TDS concentration go?
The system can concentrate high-salinity wastewater from tens of thousands mg/L to over 210,000 mg/L, approaching the saturation point of sodium chloride.
Is the system easy to install?
Yes, the system features a standard containerized skid-mounted design, allowing for rapid on-site deployment within 1 to 7 days and easy relocation between different sites.
Can I recover usable resources from my wastewater?
Absolutely. By integrating nanofiltration salt separation, you can recover industrial-grade sodium chloride and sodium sulfate, turning waste into profitable by-products.
What capacities are available?
We offer a full range of capacities from 0.5 m³/h up to 500 m³/h, and multiple units can be connected in parallel for even larger industrial park requirements.
Does the system require manual supervision?
The system is equipped with PLC intelligent control and real-time online monitoring, supporting unattended continuous operation with automated alarms.

Related Products