OEM High-Salinity Wastewater Treatment System - ZLD Solutions from China Suppliers and Factory Suppliers, Manufacturers

,

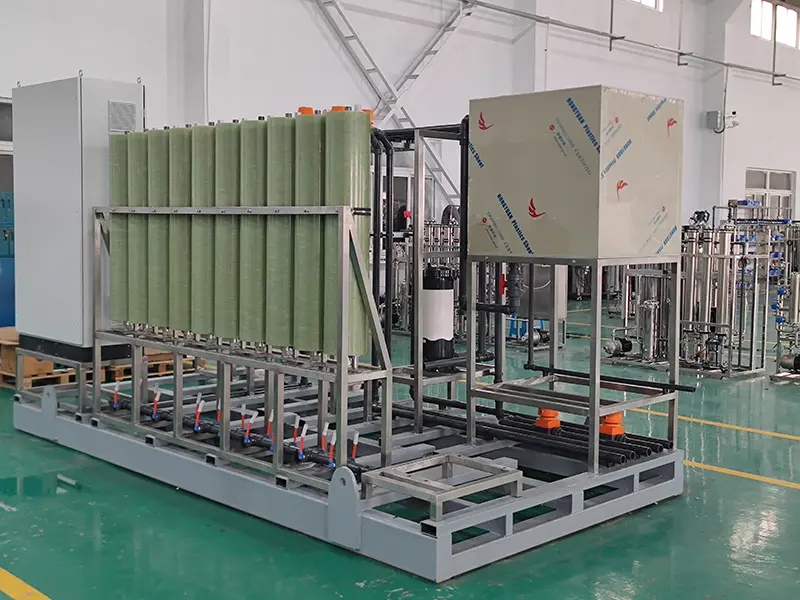
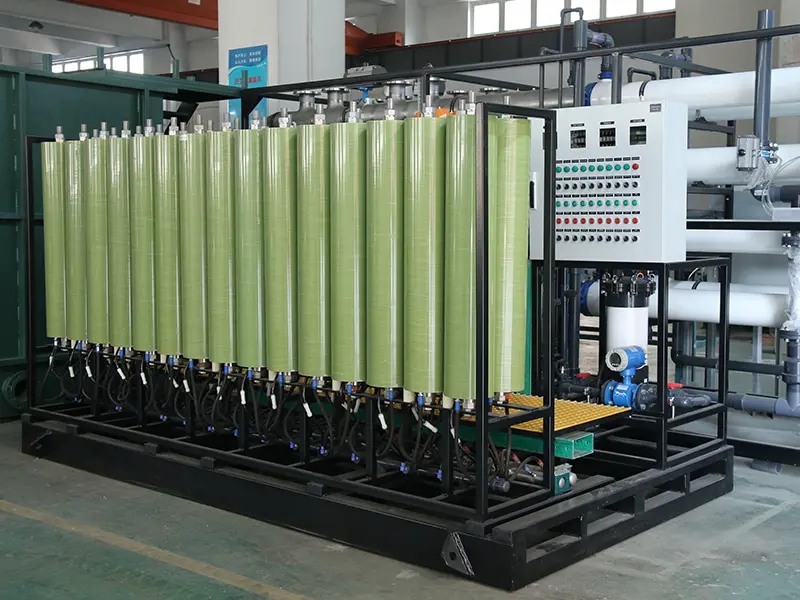
OARO Membrane System for High-Salinity Wastewater Treatment

,

Introducing the OARO membrane system, an innovative solution specifically tailored for high-salinity wastewater treatment. This advanced system, manufactured in China, employs cutting-edge evaporation and crystallization technologies to deliver significant reductions in wastewater volume, effectively lowering treatment costs for various industries, including chemical, pharmaceutical, and electroplating. As a leading choice among suppliers and factories, the OARO system boasts fully automated operation, low energy consumption, and a compact design, enabling facilities to achieve near-zero liquid discharge with ease. Its reliability and durability support enterprises in meeting regulatory standards while promoting a shift towards environmentally-friendly production practices.

,

Product Description

✓Our Solution

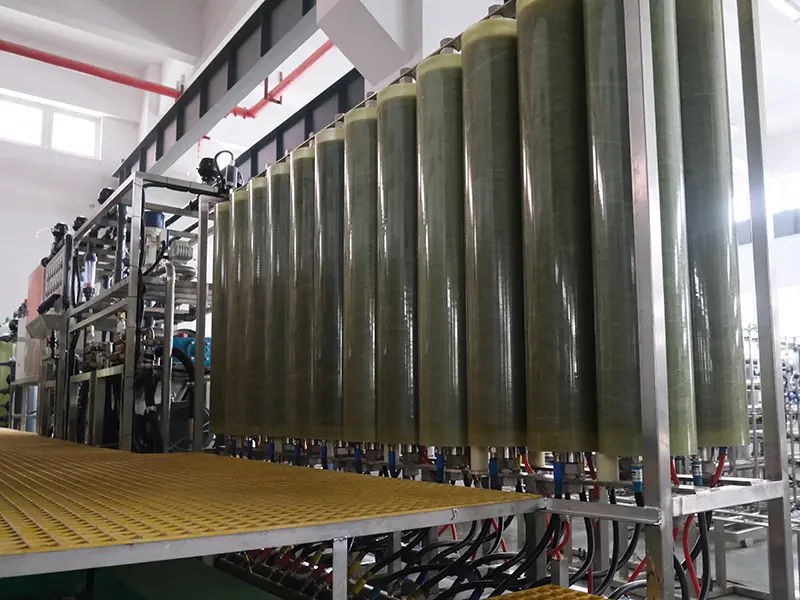
Shanghai Tongjie Environmental Protection's high-salt wastewater reduction and resource recovery system employs a combined process of OARO (Optical Advanced Reverse Osmosis) for high-salt concentration, DTRO (Dialysis-Treated Reverse Osmosis) for high-pressure reverse osmosis, and MVR (Membrane Vapor Recovery) for evaporation and crystallization. The raw water has a TDS concentration of 10,000–50,000 ppm, which is concentrated to over 150,000 ppm TDS, achieving zero wastewater discharge and salt resource recovery.

Adapted for: Chemical engineering, electroplating, lithium salts, coal chemical industry, pharmaceuticals, and printing and dyeing.

★Core Advantages
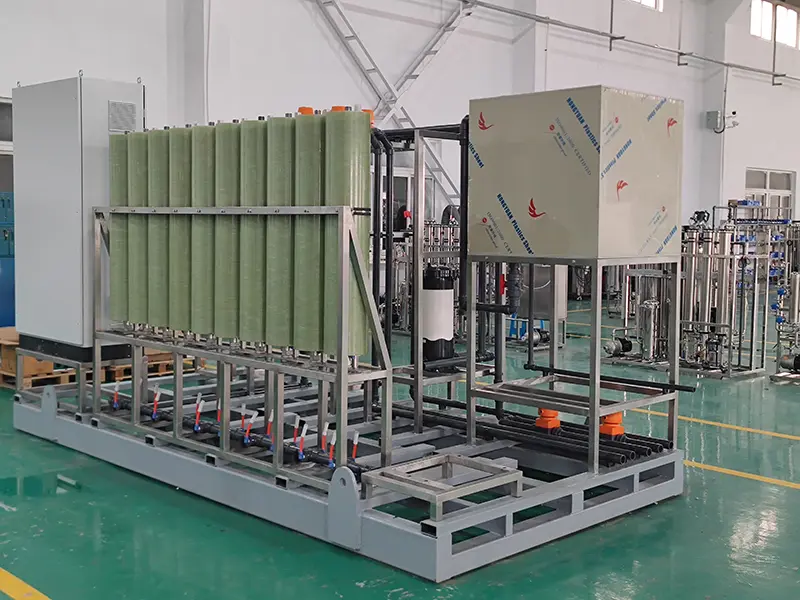
STRO System
DTRO System
📈
High concentration ratio and reduction rate:

The combination of pretreatment + OARO reduces the concentrated water volume by 80–90%, significantly decreasing the evaporation scale.

🏗️
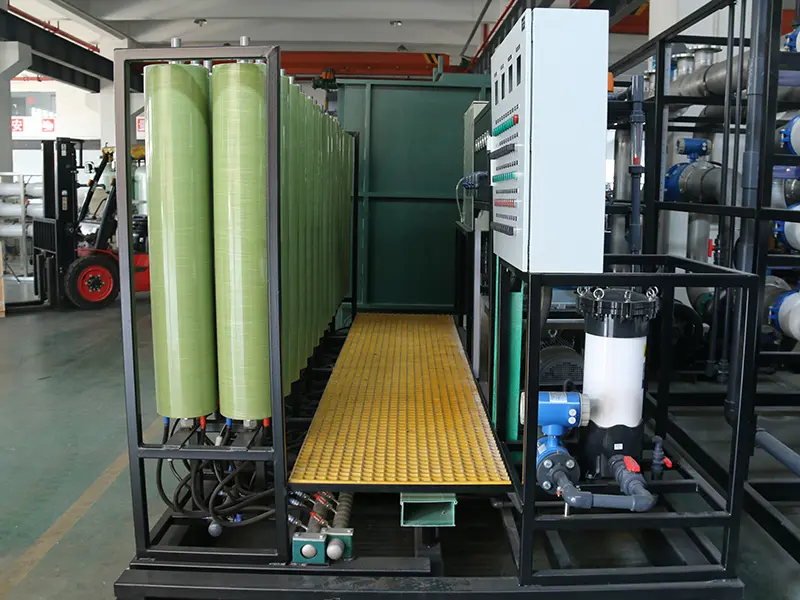
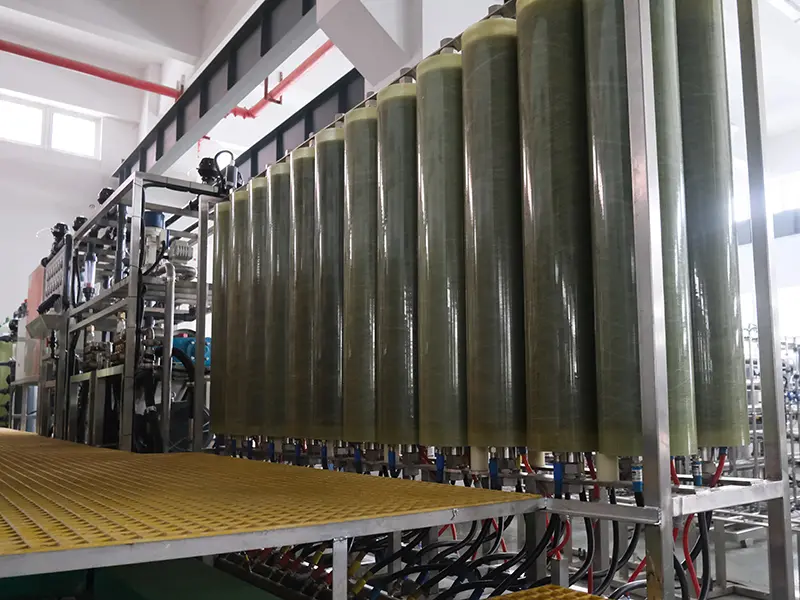
Modular skid-mounted design:

Enables rapid factory prefabrication and on-site commissioning within 30 days, reducing civil construction by 60% while allowing phased expansion.

⚡
Energy conservation and cost reduction:

Energy consumption is reduced by 40%. Membrane concentration replaces partial evaporation, with energy consumption per ton of water ≤0.8 kWh, resulting in a 30% reduction in operating costs.

🛡️
Pollution-resistant and scale-preventing:

Long-lasting stable wide-channel anti-pollution membrane + softening pretreatment, tolerant to high hardness/high COD, with cleaning cycle extended by 3 times.

An ideal solution for meeting short-term or long-term decentralized water supply demands

Contact Now

⚙Core Technical Parameters

Inlet TDS 10,000–50,000 ppm
After concentration, TDS 150,000 ppm+
Processing capacity 50–5000 tons/day (customizable)
Process Pretreatment + OARO + MVR

🎯Application Scenarios

Lithium salt industry: Brine from salt lakes and lithium mining wastewater.
Chemical Industry: High-salt organic wastewater and evaporation liquor reduction.
Electroplating/Textile: Heavy metal-containing and dye concentrate wastewater.
Pharmaceuticals: Fermentation high-salt wastewater with zero discharge.
Mineral water: High-salinity mine water for salt resource recovery.

?Frequently Asked Questions

Can high COD levels (2000 ppm) be treated?
By employing a coupled "pre-treatment + membrane separation" technology, the COD removal rate exceeds 90%, allowing direct feed into the membrane system.
Can lithium extraction from concentrated water achieve industrial-grade purity?
The specialized lithium extraction process yields lithium salts with a purity of ≥99%, directly meeting battery-grade and industrial-grade requirements.
Is system scaling severe?
With chemical softening, anti-fouling membrane, and online cleaning, the scaling risk is reduced by 80%, ensuring long-term stable operation.
What is the typical timeframe for project implementation?
Thanks to our modular skid-mounted design, factory prefabrication and on-site commissioning can be completed within 30 days.
How much energy can be saved compared to traditional evaporation?
Our system reduces energy consumption by 40% using membrane concentration to replace partial evaporation, with energy usage ≤0.8 kWh per ton.
What is the maximum TDS concentration achievable?
Our OARO and DTRO combined process can concentrate raw water from 10,000 ppm up to over 150,000 ppm TDS.

❖Other Products

Modular Seawater Desalination

Modular Containerized Seawater Desalination
ZLD System

High-Salinity Wastewater ZLD System

OEM Manufacturing

OEM Precision Manufacturing

Innovation

ODM Full Value Chain Innovation

✉Send Inquiry

Related Products