
Wholesale China Deoxygenation Membrane Equipment Supplier - Factory for Physical Degassing to Remove Dissolved Oxygen Factories, Manufacturer
Product Description
Working Principle
The core working principle of the deoxygenation membrane equipment is based on Henry's Law and the gas-liquid mass transfer process. Henry's Law states that at a constant temperature, the equilibrium concentration of a dissolved gas in a liquid is directly proportional to the partial pressure of that gas in the gas phase.
The equipment uses a hydrophobic microporous hollow fiber membrane as the gas-liquid contact interface, creating a dissolved oxygen concentration gradient across the membrane that drives oxygen molecules to migrate from the liquid phase to the gas phase.
The membrane material is selected from hydrophobic polymers such as polypropylene (PP) or polyvinylidene fluoride (PVDF). The pore size of the membrane micro-pores ranges from 0.01 to 0.1 micrometers.
The hydrophobic nature prevents the water phase from penetrating the membrane pores, while gas molecules dissolved in the water can freely pass through the membrane pores into the gas phase side.
The equipment provides two flexible operating process modes designed for high-efficiency dissolved oxygen removal.
Vacuum Deoxygenation Mode
A vacuum pump creates a negative pressure environment on the gas phase side of the membrane module, bringing the oxygen partial pressure on the gas phase side close to zero. Water containing dissolved oxygen flows on the liquid phase side of the membrane module. Driven by the partial pressure difference, oxygen molecules pass through the membrane pores into the gas phase side and are continuously discharged by the vacuum pump. In this mode, the outlet dissolved oxygen concentration can be reduced to below 1 μg/L.
High-Purity Nitrogen Sweep Mode
High-purity nitrogen gas (purity ≥ 99.999%) is introduced into the gas phase side of the membrane module as a sweep gas. The high-purity nitrogen maintains an extremely low oxygen partial pressure on the gas phase side. Driven by the concentration gradient, dissolved oxygen in the liquid phase passes through the membrane pores into the gas phase side and is discharged along with the sweep gas. In this mode, the outlet dissolved oxygen concentration can be reduced to below 5 μg/L.
The two modes can be selected based on actual operating conditions. The vacuum mode is suitable for applications with strict requirements for outlet dissolved oxygen levels; the nitrogen sweep mode is suitable for sites with a stable supply of nitrogen. The equipment can operate within a temperature range of 5 to 40 degrees Celsius, with an inlet water pressure range of 0.1 to 0.5 MPa.
Equipment Structure and Core Components
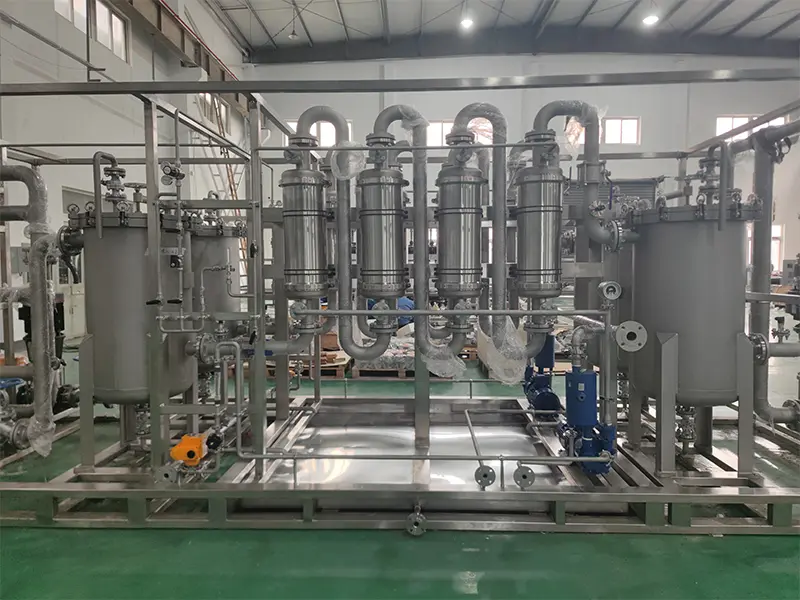
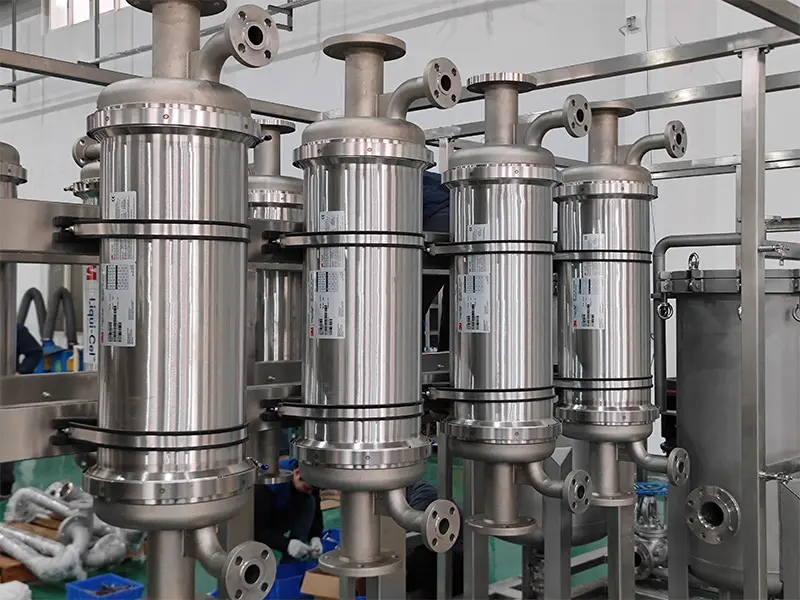
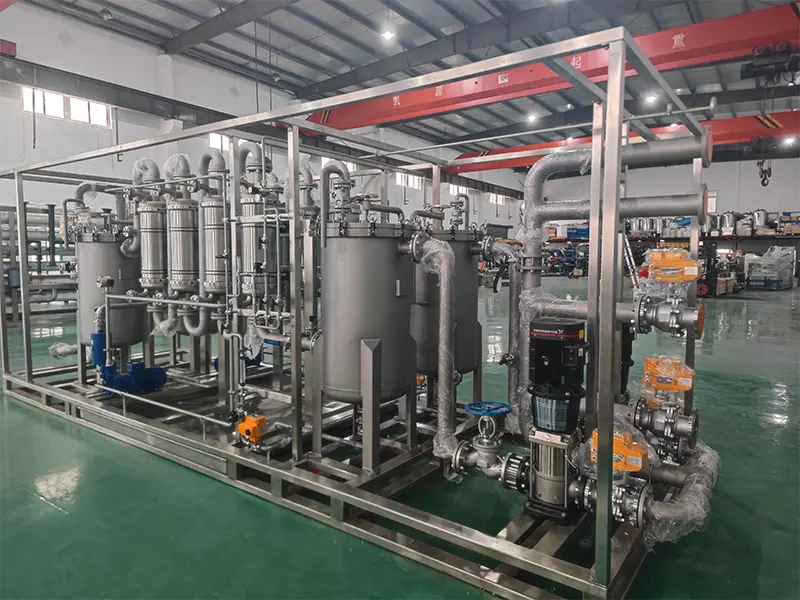
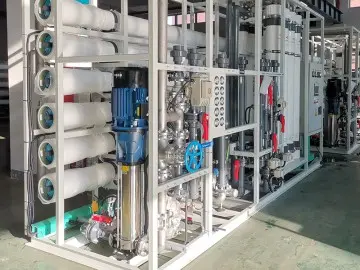
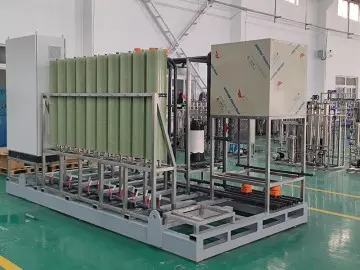
The deoxygenation membrane equipment consists of a membrane contactor unit, a vacuum system or sweep gas system, and piping and control systems. The membrane contactor is the core component of the equipment, internally packed with hollow fiber membranes arranged in bundles, with both ends potted and fixed using epoxy resin, and the whole assembly enclosed in a stainless steel or engineering plastic housing. The housing has four ports: two for the liquid phase and two for the gas phase.
The liquid phase side is equipped with an inlet and an outlet. Water flows either inside or outside the membrane fibers, resulting in either an inside-out or outside-in flow path design depending on the membrane module configuration. The gas phase side is equipped with a vacuum port or sweep gas inlet/outlet ports. The vacuum mode is equipped with a liquid-ring or rotary vane vacuum pump; the sweep mode is connected to a nitrogen supply line. The control system includes flow control valves, pressure gauges, vacuum indicators, and online dissolved oxygen monitors for real-time monitoring of equipment operating parameters.
System Process Flow
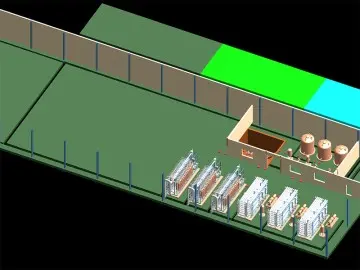
The deoxygenation membrane system is connected in series after the Reverse Osmosis (RO) or Electrodeionization (EDI) module. Process flow: RO/EDI permeate enters the feed pump, is pressurized, and sent to the shell side of the deoxygenation membrane, producing deoxygenated water. The auxiliary system consists of a vacuum unit and a sweep gas unit. The vacuum system includes a liquid-ring vacuum pump or dry screw vacuum pump, a gas-liquid separation tank, and a circulating water tank; the sweep gas system includes nitrogen cylinders, a pressure reducing valve, and a mass flow controller.
For conditions requiring product water dissolved oxygen below 5 ppb, a two-stage series process is used: the first stage membrane tube side is connected to a vacuum pump, and the second stage membrane tube side uses nitrogen sweep combined with vacuum. The inlet water quality must meet: turbidity < 1 NTU, total suspended solids < 5 mg/L, residual chlorine < 0.1 ppm, to prevent membrane surface fouling and blockage, as well as oxidative degradation of the polypropylene material. The PLC control system collects data on inlet flow rate and product water dissolved oxygen, and uses PID algorithms to adjust the vacuum pump frequency and sweep gas flow rate, maintaining product water quality while reducing operating energy consumption.
Application Fields
Other Products
Modular Containerized Seawater De...
Seawater desalting equipment
High-Salinity Wastewater Volume R...
OEM Precision Manufacturing
ODM Full Value Chain Innovation
Water Reuse Equipment (Pretreatme...
Water Reuse Equipment High-Ratio ...
Industrial Demineralized Water Eq...
Send Inquiry
Frequently Asked Questions
What dissolved oxygen (DO) levels can be achieved with this membrane equipment?
Under vacuum deoxygenation mode, dissolved oxygen can be reduced to below 1 μg/L (ppb). Under high-purity nitrogen sweep mode, it can achieve below 5 μg/L. Using a two-stage series system combining vacuum and nitrogen sweep, DO levels can be maintained consistently below 5 ppb.
How do I choose between Vacuum Mode and Nitrogen Sweep Mode?
Vacuum mode is ideal for installations where ultra-low DO (below 1 μg/L) is required without gas consumption. The nitrogen sweep mode is optimal for facilities with an existing, stable high-purity nitrogen (≥ 99.999%) supply.
What are the required feed water quality conditions?
The system requires inlet water turbidity < 1 NTU, total suspended solids (TSS) < 5 mg/L, and residual chlorine < 0.1 ppm. Feed water is typically pre-treated via RO (Reverse Osmosis) or EDI (Electrodeionization) systems.
What are the typical operating pressure and temperature limits?
The equipment operates efficiently in an inlet water pressure range of 0.1 to 0.5 MPa and within a temperature window of 5°C to 40°C.
What membrane materials are used and what is the pore size?
The hollow fiber membranes are manufactured from hydrophobic polymers like Polypropylene (PP) or Polyvinylidene Fluoride (PVDF) with micro-pore sizes ranging from 0.01 to 0.1 micrometers.
Can membrane deoxygenation replace chemical deaeration in boilers?
Yes. Membrane contactor deoxygenation replaces conventional thermal deaerators and chemical oxygen scavengers (like hydrazine or sodium sulfite), eliminating chemical handling, reducing thermal energy loss, and lowering operating costs.









