Wholesale High-Salinity Wastewater Treatment System Factory in China: OARO Membrane Solutions from Reliable Suppliers Factory, Manufacturer

,

OARO Membrane System

,

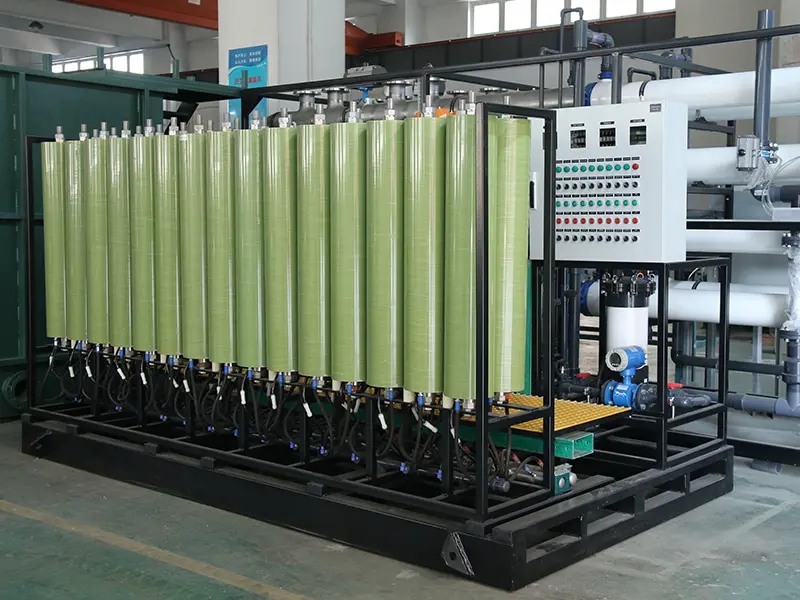
The OARO membrane system is an innovative solution specifically designed for high-salinity wastewater treatment. This advanced system utilizes cutting-edge evaporation and crystallization technologies to significantly reduce wastewater volume and lower treatment costs, making it an ideal choice for industries such as chemical, pharmaceutical, and electroplating. As a leading China supplier, we provide this fully automated system that boasts low energy consumption and a compact footprint, enabling near-zero liquid discharge. With its reliable and durable performance, the OARO system supports factories in meeting regulatory standards and advancing toward sustainable green production practices. Choose OARO for effective wastewater management and environmental compliance.

,

Product Description

🌀 Our Solution

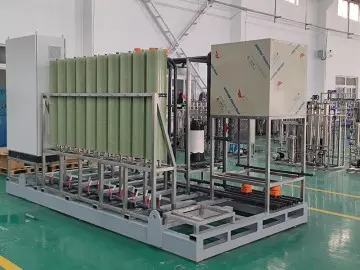
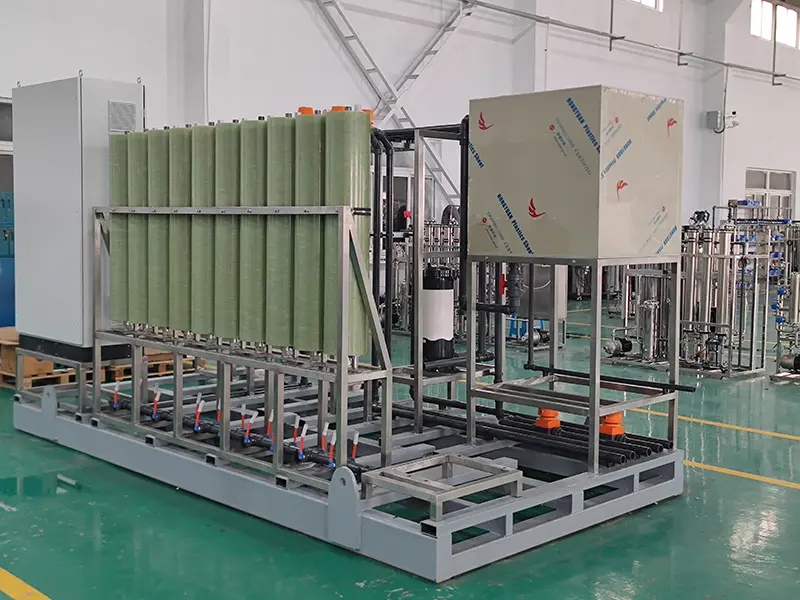
Shanghai Tongjie Environmental Protection's high-salt wastewater reduction and resource recovery system employs a combined process of OARO (Optical Advanced Reverse Osmosis) for high-salt concentration, DTRO (Dialysis-Treated Reverse Osmosis) for high-pressure reverse osmosis, and MVR (Membrane Vapor Recovery) for evaporation and crystallization. The raw water has a TDS concentration of 10,000–50,000 ppm, which is concentrated to over 150,000 ppm TDS, achieving zero wastewater discharge and salt resource recovery.

Adapted for high-salt industries such as chemical engineering, electroplating, lithium salts, coal chemical industry, pharmaceuticals, and printing and dyeing.

⭐ Core Advantages
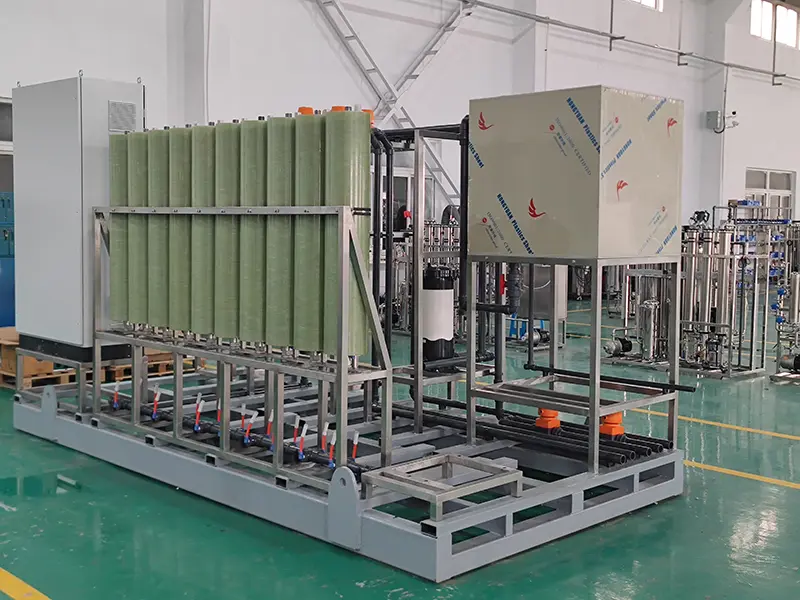
STRO System
1. High concentration ratio and reduction rate:

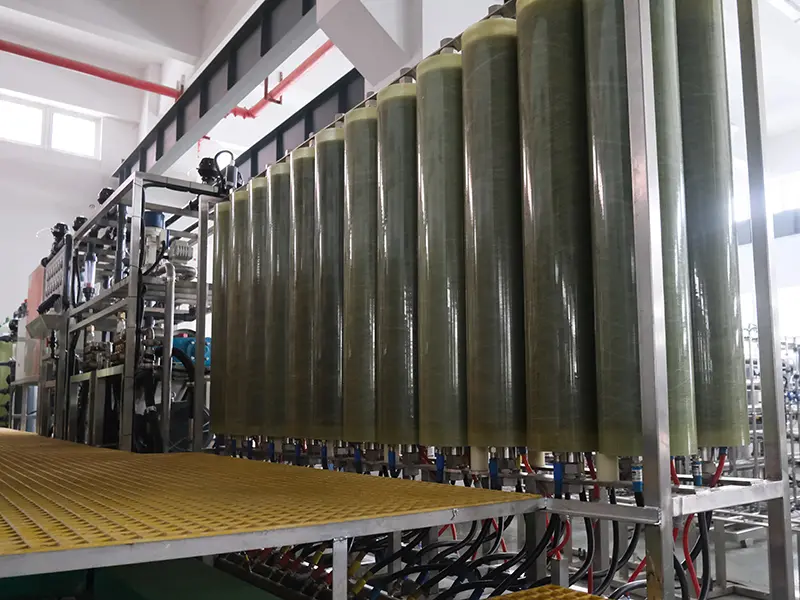
The combination of pretreatment + OARO reduces the concentrated water volume by 80–90%, significantly decreasing the evaporation scale.

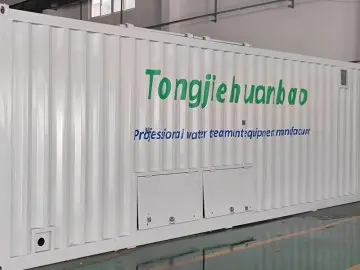
2. Modular skid-mounted design:

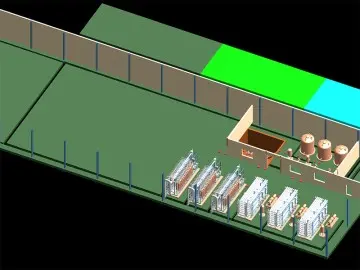
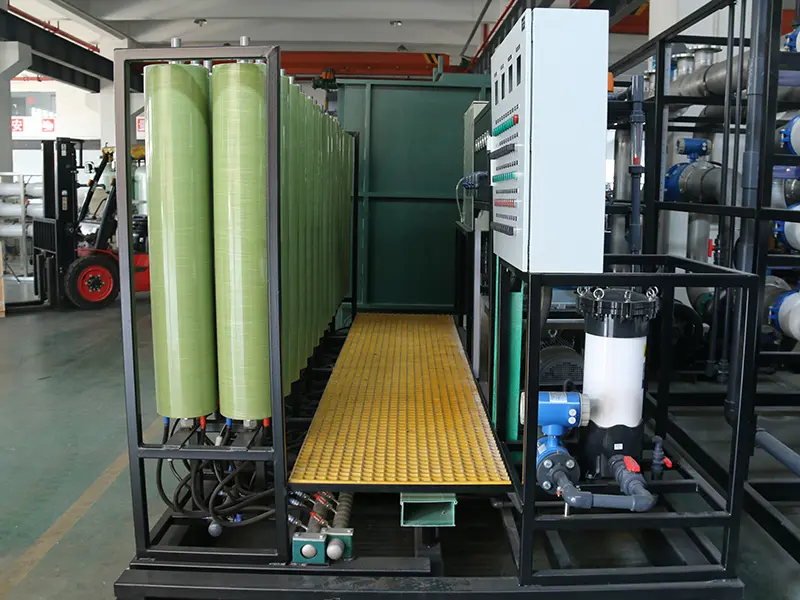
Enables rapid factory prefabrication and on-site commissioning within 30 days, reducing civil construction by 60% while allowing phased expansion.
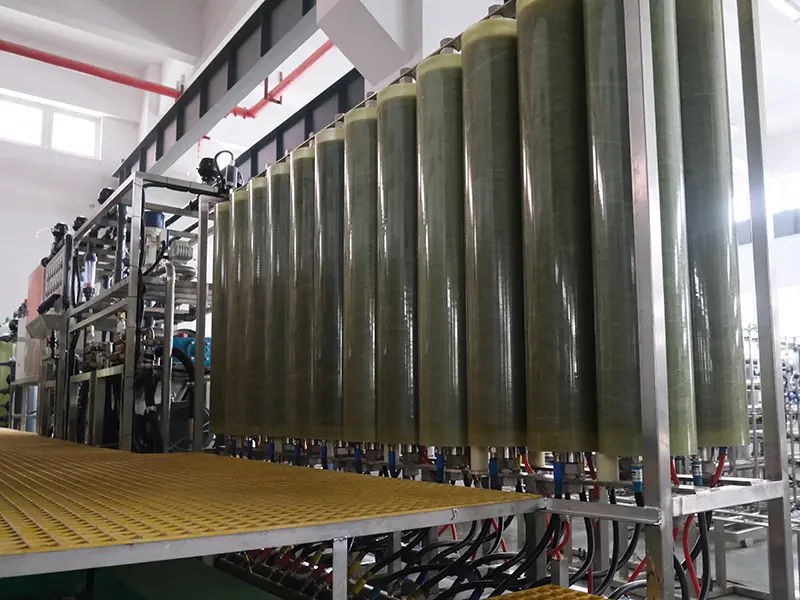
DTRO System
3. Energy conservation and cost reduction:

Energy consumption is reduced by 40%. Membrane concentration replaces partial evaporation, with energy consumption per ton of water ≤0.8 kWh, resulting in a 30% reduction in operating costs.

4. Pollution-resistant and scale-preventing:

Long-lasting stable wide-channel anti-pollution membrane + softening pretreatment, tolerant to high hardness/high COD, with cleaning cycle extended by 3 times.

An ideal solution for meeting short-term or long-term decentralized water supply demands

📊 Core Technical Parameters

Inlet TDS 10,000–50,000 ppm
After concentration, TDS 150,000 ppm+
Processing capacity 50–5000 tons/day (customizable)
Process Pretreatment + OARO + MVR

🚀 Application Scenarios

◈ Lithium salt industry: Concentration of brine from salt lakes and mining processes.
◈ Chemical Industry: High-salt organic wastewater, reduction of evaporation mother liquor.
◈ Electroplating/Textile: Heavy metal-containing high-salt wastewater, dye concentrate.
◈ Pharmaceuticals: Fermentation of high-salt wastewater with zero discharge.
◈ Mineral water: High-salinity mine water for salt resource recovery.

📦 Other Products

Seawater Desalination
Modular Seawater Desalination
ZLD System
Wastewater ZLD System
OEM Manufacturing
OEM Precision Manufacturing

❓ FAQ

Can high COD levels (2000 ppm) be treated?
By employing a coupled "pre-treatment + membrane separation" technology, the COD removal rate exceeds 90%, allowing direct feed into the membrane system.
Can lithium extraction from concentrated water achieve industrial-grade purity?
The specialized lithium extraction process yields lithium salts with a purity of ≥99%, directly meeting battery-grade and industrial-grade requirements.
Is system scaling severe?
With chemical softening, anti-fouling membrane, and online cleaning, the scaling risk is reduced by 80%, ensuring long-term stable operation.
How long does the on-site commissioning take?
Thanks to our modular skid-mounted design, on-site commissioning can typically be completed within 30 days.
What is the energy consumption of the system?
Energy consumption is reduced by 40% compared to traditional methods, with energy consumption per ton of water being ≤0.8 kWh.
Which industries can benefit from this recovery system?
It is ideal for high-salt industries including chemical engineering, electroplating, lithium salts, coal chemicals, pharmaceuticals, and textile dyeing.

📧 Send Inquiry

Related Products