Wholesale High-Salinity Wastewater Volume Reduction & ZLD System Suppliers, Manufacturer
Product Description
Our Solution
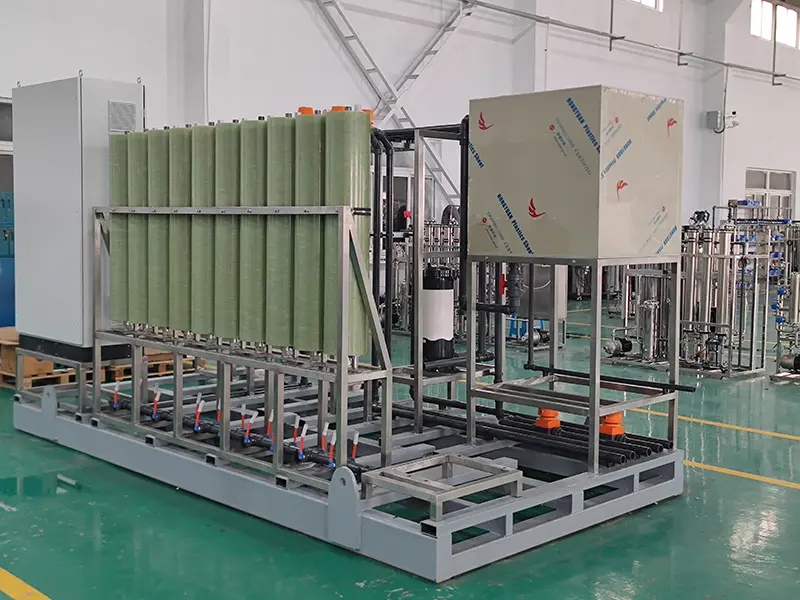
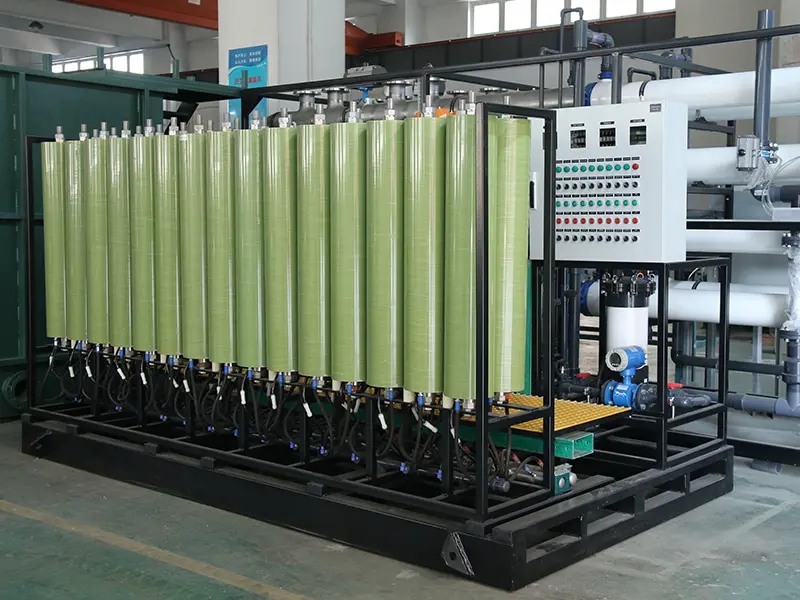
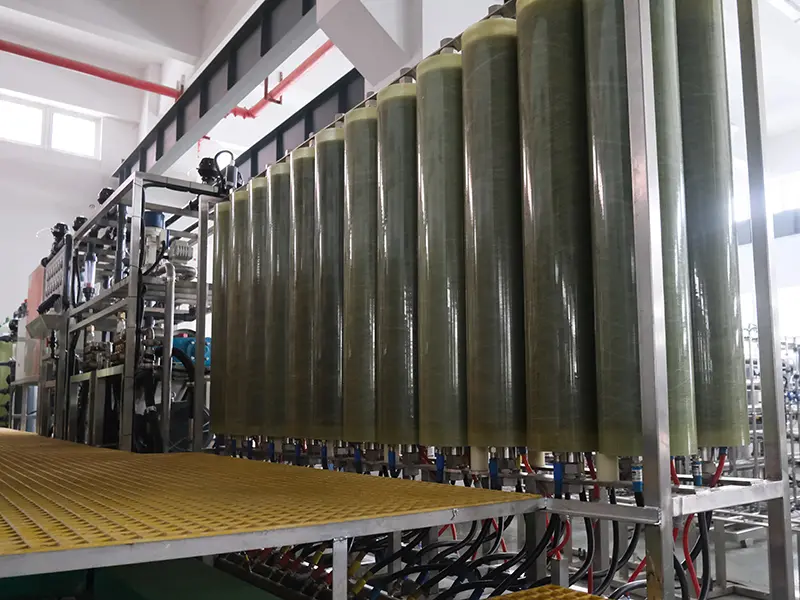
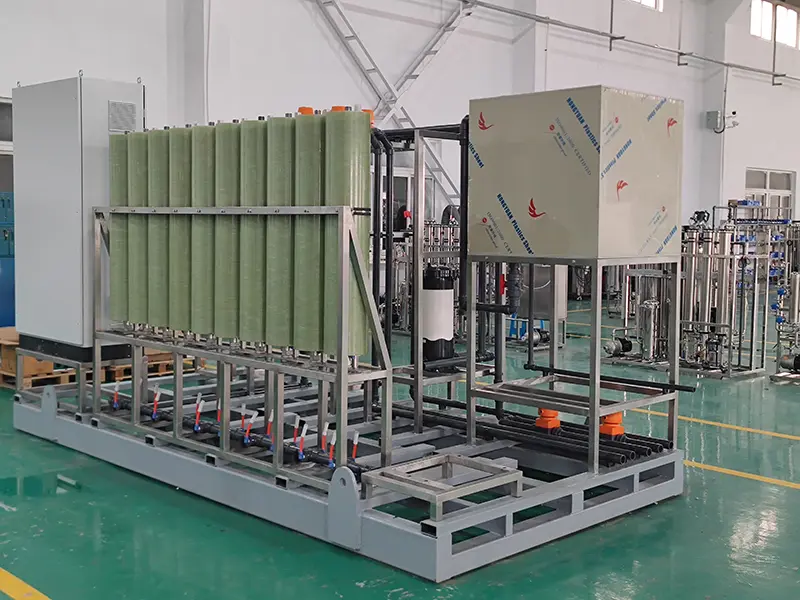
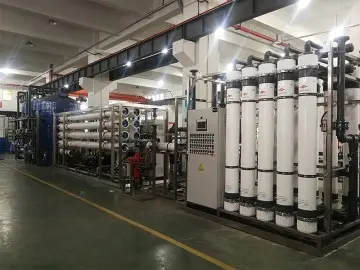
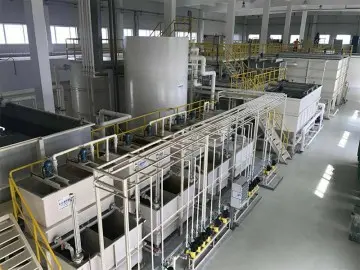
Shanghai Tongjie Environmental Protection's high-salt wastewater reduction and resource recovery system employs a combined process of OARO (Optical Advanced Reverse Osmosis) for high-salt concentration, DTRO (Dialysis-Treated Reverse Osmosis) for high-pressure reverse osmosis, and MVR (Membrane Vapor Recovery) for evaporation and crystallization. The raw water has a TDS concentration of 10,000–50,000 ppm, which is concentrated to over 150,000 ppm TDS, achieving zero wastewater discharge and salt resource recovery.
Adapted for high-salt industries such as chemical engineering, electroplating, lithium salts, coal chemical industry, pharmaceuticals, and printing and dyeing.
Core Advantages
Core Technical Parameters
| Inlet TDS | 10,000–50,000 ppm |
| After Concentration TDS | 150,000 ppm+ |
| Processing Capacity | 50–5000 tons/day (customizable) |
| Process Scheme | Pretreatment + OARO + MVR |
Application Scenarios
Frequently Asked Questions
By employing a coupled "pre-treatment + membrane separation" technology, the COD removal rate exceeds 90%, allowing direct feed into the membrane system.
The specialized lithium extraction process yields lithium salts with a purity of ≥99%, directly meeting battery-grade and industrial-grade requirements.
With chemical softening, anti-fouling membrane, and online cleaning, the scaling risk is reduced by 80%, ensuring long-term stable operation.
The system effectively processes raw water with a TDS concentration of 10,000–50,000 ppm, concentrating it to over 150,000 ppm TDS for zero discharge and salt recovery.
Energy consumption is reduced by 40% (≤0.8 kWh/ton) by replacing partial evaporation with membrane concentration, resulting in an overall operating cost reduction of 30%.
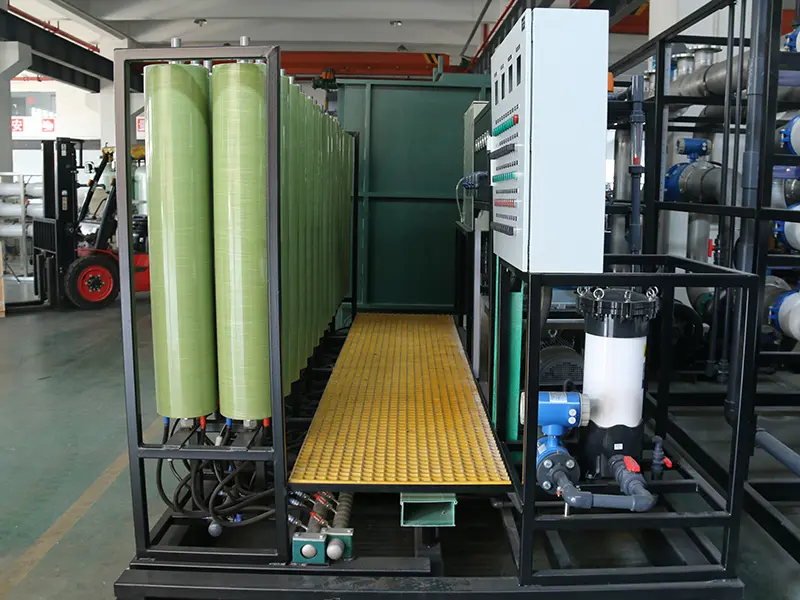
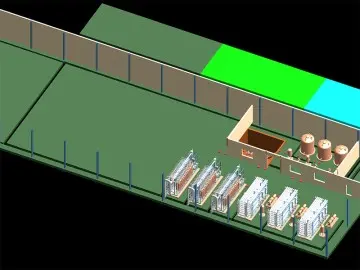
The modular skid-mounted design enables rapid factory prefabrication and on-site commissioning within 30 days while reducing civil construction requirements by 60%.
Other Products
Modular Containerized Seawater De...
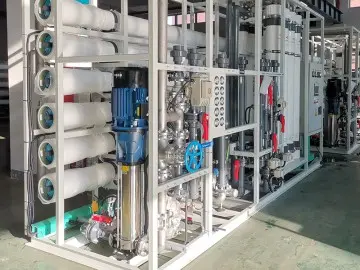
Seawater desalting equipment
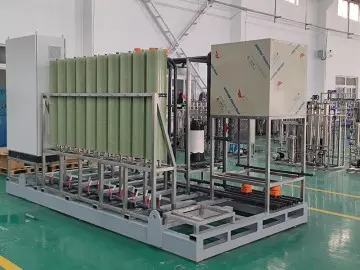
High-Salinity Wastewater Volume R...
OEM Precision Manufacturing
ODM Full Value Chain Innovation
Water Reuse Equipment (Pretreatme...
Water Reuse Equipment High-Ratio ...