
OEM Food&Beverage Process Water System Factory, Suppliers
Product Description
Product Description
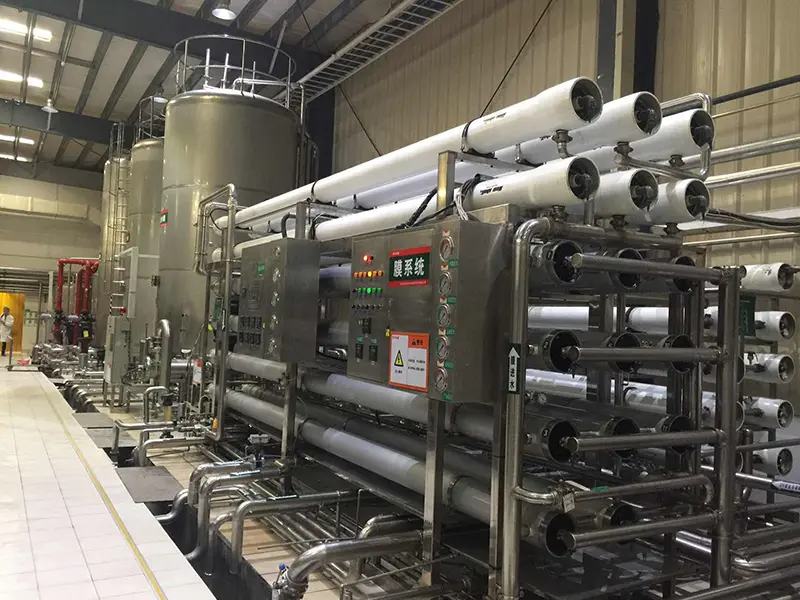
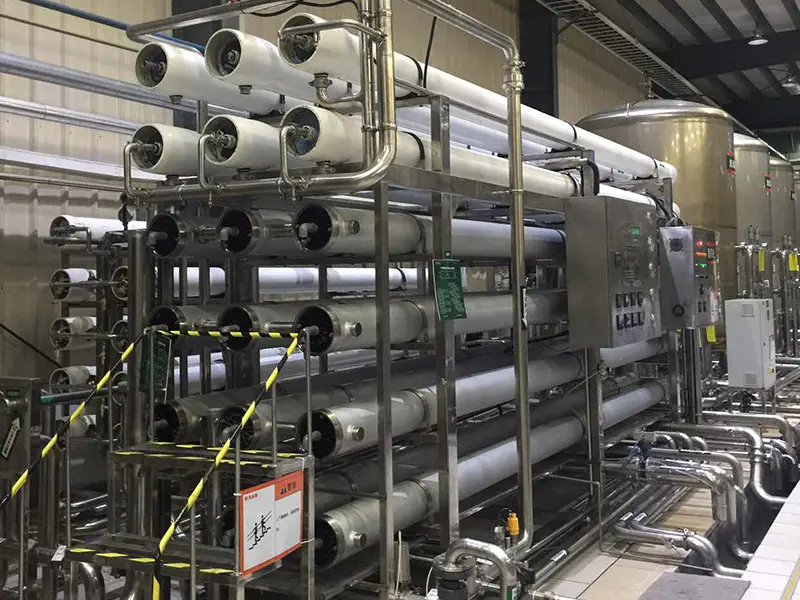
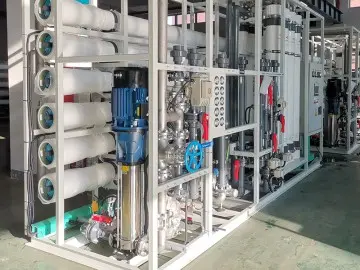
This purified water system is a complete water treatment solution designed specifically for the food & beverage industry. Built around two-stage reverse osmosis (RO), it integrates pretreatment, fine filtration, disinfection, and intelligent control — delivering “raw water in, purified water out” fully automatically.
System Specifications & Overview
Raw water → Raw water tank → Booster pump → Multimedia filter → Activated carbon filter → Water softener (optional) → Cartridge filter → 1st pass RO → 2nd pass RO → UV sterilizer / ozone generator → Stainless steel sterile pure water tank → Distribution points.
• Conductivity consistently ≤ 10 μS/cm (customisable to ≤ 1 μS/cm)
• Desalination rate ≥ 98%
• Microorganisms, heavy metals, residual chlorine fully comply with food processing & packaged drinking water standards.
1 – 100 tonnes per hour. Features a modular design for easy customisation and future expansion.
PLC fully automatic control + 7” touch screen; real-time monitoring of conductivity, flow rate, pressure, pH, etc.; remote monitoring & automatic alarm available.
Advantage Technical Highlights
| Advantage | Technical Highlights |
|---|---|
| High Desalination Rate | Two-pass RO system achieves ≥98% desalination, effectively removing dissolved salts, heavy metals, bacteria, and organic compounds. |
| Consistent Compliance | Product water conductivity can be as low as ≤1 μS/cm, meeting GB 5749, GB 19298, GB 14881, and other food safety standards. |
| High Recovery Rate | System recovery 50%~80%; concentrate can be reclaimed to save water and reduce discharge. |
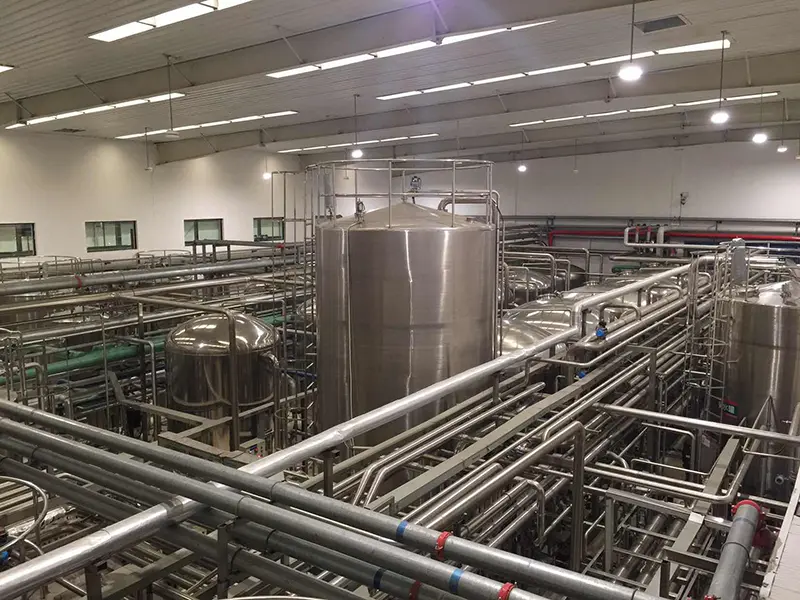
| Food Grade Materials | Piping and storage tanks made of 304/316L hygienic stainless steel, quick-connect joints, deadleg-free design, supports CIP cleaning. |
| Double Disinfection | 254 nm UV sterilisation (≥99.9% kill rate) + ozone mixing, eliminates microbial recontamination. |
| Smart Control | PLC + IoT remote monitoring; automatic alarm and discharge if water quality exceeds limit; RO membranes auto-flushed at set intervals to prolong membrane life. |
| Low Operating Cost | Energy consumption approx. 2.5–4.5 kWh/m³ produced; long consumable replacement cycle; 25%~35% lower O&M cost compared to conventional processes. |
| Flexible Customisation | Options for high-hardness water, high residual chlorine, high microbial load etc. — e.g. extra softening, enhanced activated carbon, UV+ozone combination. |
Application Areas
Other Related Products
Modular Containerized Seawater Desalination Equipment
Seawater Desalting Equipment
High-Salinity Wastewater Volume Reduction & ZLD
OEM Precision Manufacturing
ODM Full Value Chain Innovation
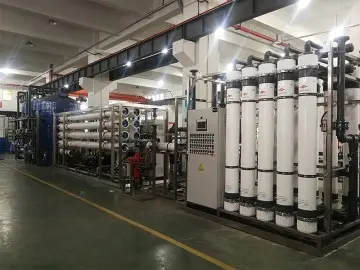
Water Reuse Equipment (Pretreatment + UF + RO)
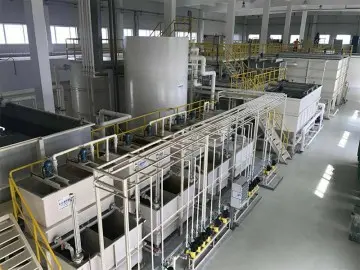
Water Reuse Equipment High-Ratio Reuse Process
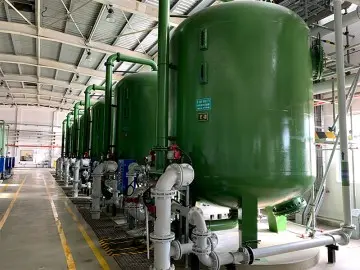
Industrial Demineralized Water Equipment
Send Inquiry
Frequently Asked Questions (FAQ)
A: The purified water system achieves a conductivity of ≤ 10 μS/cm (customisable to ≤ 1 μS/cm) and a desalination rate ≥ 98%. It fully complies with GB 5749, GB 19298, and GB 14881 standards for food processing and packaged drinking water.
A: Systems can be tailored to output between 1 to 100 tonnes per hour. The modular layout allows for straightforward setup, seamless integration, and simplified future scale-ups.
A: All components, piping, and storage tanks are constructed from food-grade 304 or 316L hygienic stainless steel with quick-connect joints and a deadleg-free design. It supports CIP cleaning and features dual disinfection via UV sterilization and ozone mixing.
A: Yes, it runs via PLC fully automatic control equipped with a 7-inch touch screen. It features real-time parameter tracking (flow rate, conductivity, pressure, pH), automated membrane flushing, and remote alarm monitoring.
A: The system offers a recovery rate between 50% and 80%, allowing concentrate reclamation to conserve water. Energy consumption ranges from 2.5 to 4.5 kWh/m³, delivering a 25% to 35% reduction in overall operation and maintenance costs.








